汽车车身螺柱焊接参数对焊接组织与性能影响的研究分析
2021-11-23靳延鹏卢文超陆勇季良赵洪生孔德群
靳延鹏 卢文超 陆勇 季良 赵洪生 孔德群
摘 要:本文研究了汽车车身螺柱焊接工艺参数对焊接质量的影响,以0.8mm厚的CR3镀锌板为基体材料,采用3700号螺柱焊钉进行焊接试验,重点分析了不同焊接电流对焊接质量的影响。本文利用拉伸试验仪、分析了焊接后的焊接质量,利用金相显微镜对显微组织进行了分析研究。研究结果表明:在0.8mm厚的镀锌板进行螺柱焊接时,在提升高度为0.8mm情况下,最优的焊接电流为-800mA,焊接时间为50ms;其抗拉力为3.56KN。
关键词:汽车车身 螺柱焊 显微组织 力学性能
Research and Analysis of the Influence of Auto Body Stud Welding Parameters on Welding Structure and Performance
Jin Yanpeng Lu Wenchao Lu Yong Ji Liang Zhao Hongsheng Kong Dequn
Abstract:This paper studies the influence of welding process parameters of automobile body studs on welding quality. With 0.8mm thick CR3 galvanized sheet as the base material, 3700 stud welding studs are used for welding experiments. The article focuses on the analysis of the impact of quality of different welding currents. In this paper, the tensile tester is used to analyze the welding quality after welding, and the microstructure is analyzed and researched using a metallurgical microscope. The research results show that when stud welding is performed on a 0.8mm thick galvanized sheet, when the lifting height is 0.8mm, the optimal welding current is -800mA, the welding time is 50ms, and its tensile strength is 3.56KN.
Key words:car body, stud welding, microstructure, mechanical properties
1 试验材料及方法
1.1 试验材料
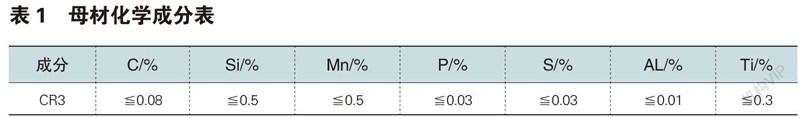
本次实验所用螺柱焊接板材材料为CR3镀锌钢板,板厚为0.8mm,其主要化学成分见表1;螺柱焊钉为3700钢钉。
1.2 试验参数
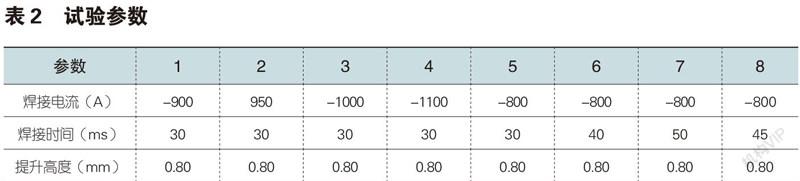
本实验采用正交实验方法,将焊接时间和焊接电流作为变量,对比相同电流和提升高度下,不同焊接时间对焊接质量的影响;对比相同焊接时间和提升高度下,不同焊接电流对焊接质量的影响。焊接电流由-800A到-1100A,焊接時间由30ms到50ms递增,实验参数如表2所示:
2 组织结构分析
2.1 微观组织分析
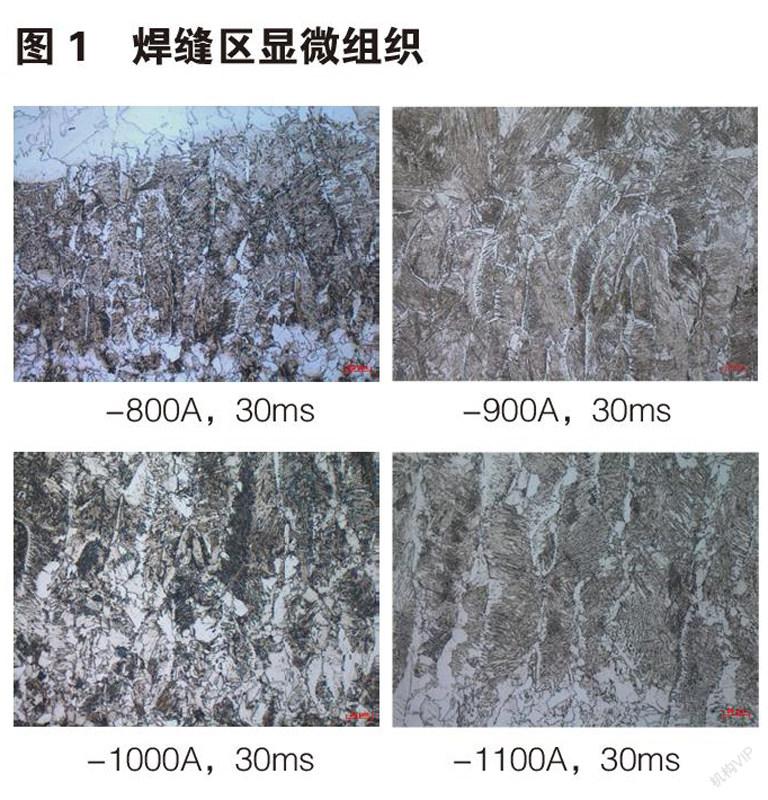
焊缝区组织相较于母材发生了很大变化,如图1所示,焊缝区组织呈板条状分布,该组织为熔融金属在焊后的快速冷却过程中形成的非平衡组织马氏体。
不同参数下,各个焊缝熔化区的组织形貌基本相似,都是板条状的马氏体,但是马氏体的分布区域相差较大。螺柱焊焊接过程中,螺钉及板材迅速升温,部分熔化,形成金属液,加热过程结束后,金属液迅速冷却,形成非平衡组织马氏体。……
