面向广义动态加工空间的机床切削稳定性研究
2020-05-21邓聪颖冯义赵洋魏博
邓聪颖 冯义 赵洋 魏博
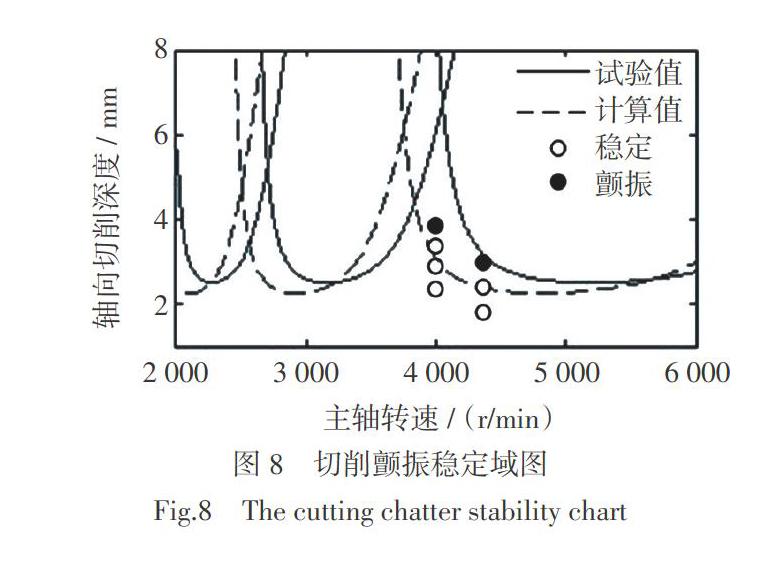
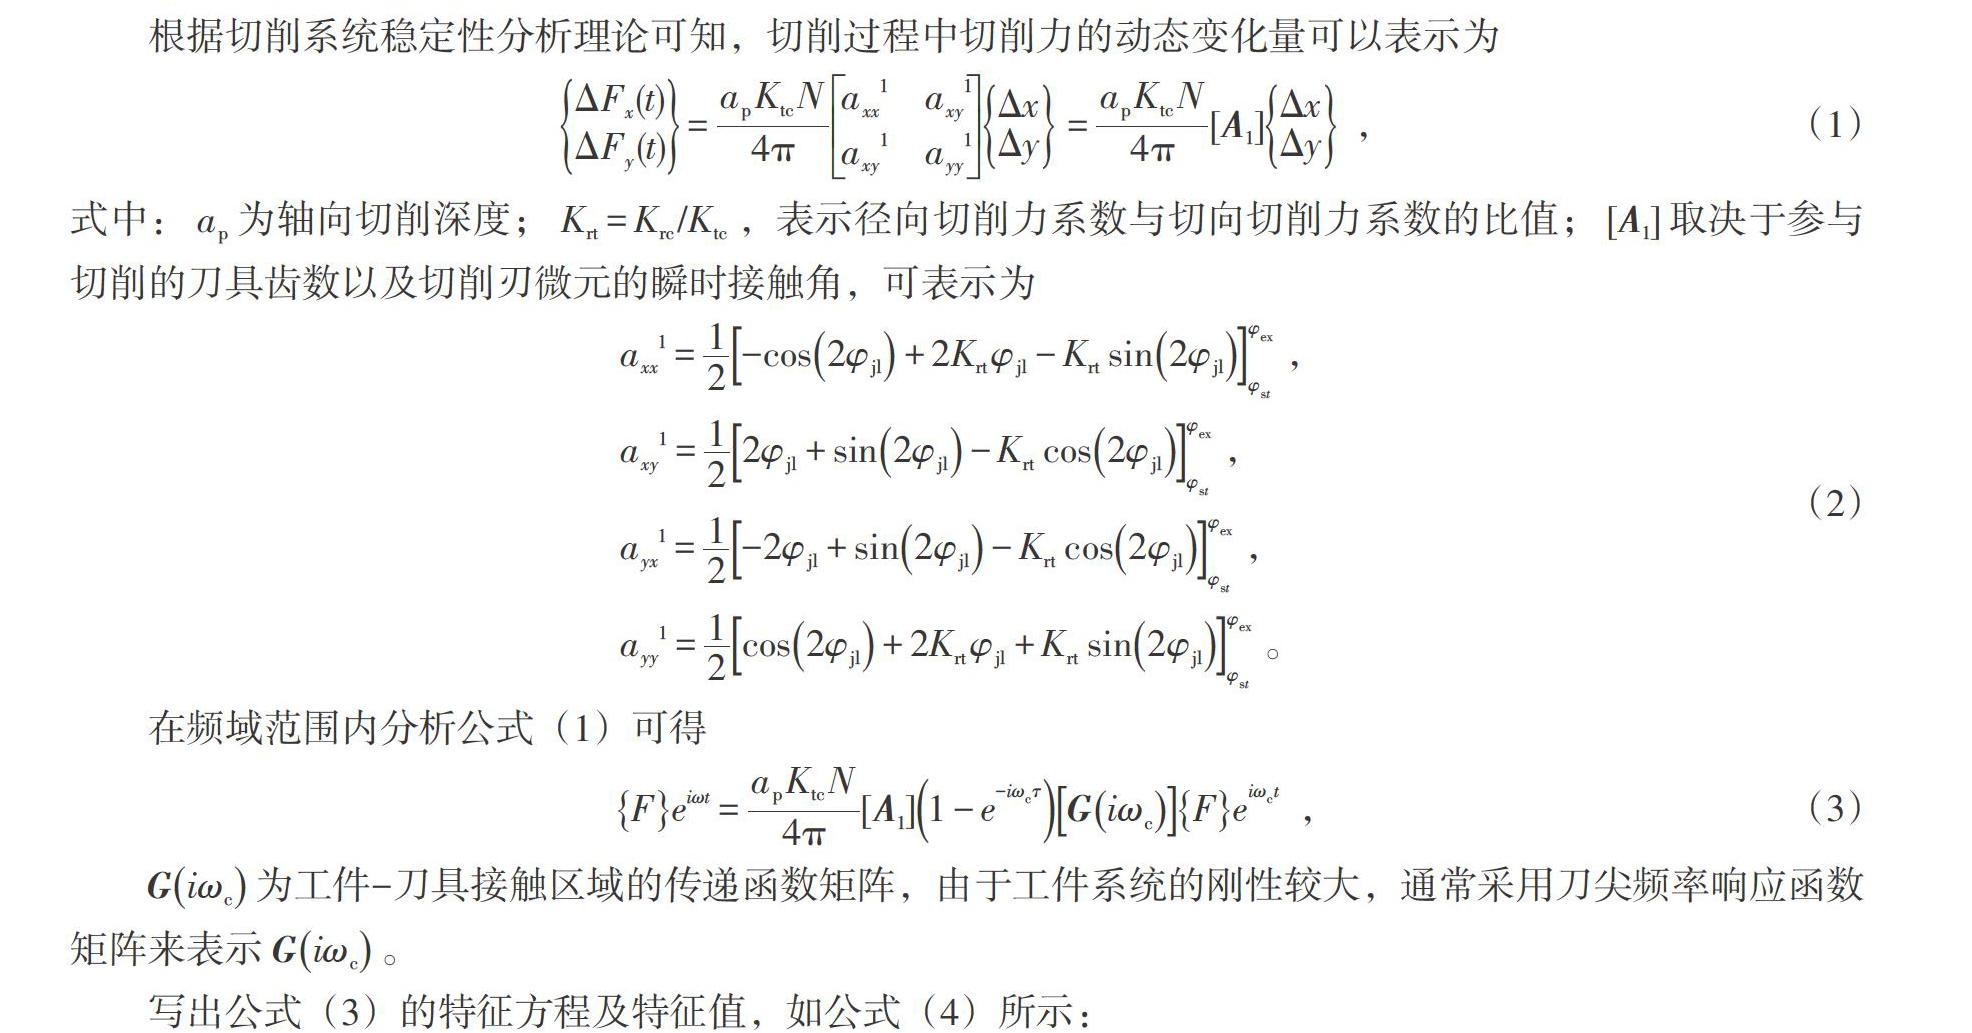

摘要 为了研究加工过程中变化的刀尖频响函数导致机床切削参数选择的不确定性,以主轴转速与运动部件位置为研究对象,提出基于广义动态空间的机床切削稳定性研究方法。该方法结合切削颤振理论与切削试验,推导工况下刀尖频响函数计算公式,通过引入正交试验法规划切削试验方案,确定主轴转速与运动部件位置对切削稳定性的影响程度以及最优参数组合,同时计算刀尖频响函数研究机床处于不同转速及位置的颤振稳定域图预测。将该方法运用于某型立式加工中心,识别主轴转速与主轴箱Z向进给位置显著影响切削稳定性,并确定刀具最优姿态,通过计算刀尖频响函数绘制颤振稳定域图,结合切削试验验证了该方法的有效性,为实际加工合理选择切削参数提供技术支持。
关 键 词 切削稳定性;频率响应函数;稳定域图;正交试验;广义动态空间
中图分类号 TG506 文献标志码 A
Research on machine tool cutting stability in the generalized dynamic space
DENG Congying1, 2, FENG Yi1, ZHAO Yang1, WEI Bo1
(1. School of Advanced Manufacturing Engineering, Chongqing University of Posts and Telecommunications, Chongqing 400065, China; 2.School of Mechanical Engineering, Chongqing University, Chongqing 400030, China)
Abstract A method to study the machine tool cutting stability is proposed in generalized dynamic space, which takes the spindle speed and moving parts positions as the objectives, for the variable in-process tool point frequency response functions (FRFs) cause uncertain choices for the cutting parameters. This method combines chatter theory and cutting experiment to derive the formulas to calculate tool point FRF and introduce orthogonal experiment method to arrange the cutting experiment. Thus, the influencing degree of the variables and their optimal combination are determined. Also these tool point FRFs are recalculated to study the cutting stability chart prediction. Applying this method in a vertical machining center, the spindle speed and Z direction displacement were identified to affect the cutting stability mostly, and the best working state for tool was determined. The stability chart was plotted by adopting the recalculated tool point FRF, from which the cutting parameters were chosen to conduct the cutting experiments. The results verify the effectiveness of the proposed method, which lays a technical support for choosing reasonable cutting parameters in machining process.
Key words cutting stability; frequency response function; chatter stability chart; orthogonal experiment; generalized dynamic space
切削加工的不穩定性严重影响机床的加工质量和切削效率,加速机床与刀具的磨损和精度的丧失[1]。机床加工时,由于断续切削、机床自身状况等因素的影响,导致刀具相对工件表面产生周期性的振动,诱发颤振,严重恶化加工零件的尺寸精度和表面质量,使切削难以继续进行[2-5]。切削稳定性与机床动力学特性密切相关,加工过程中刀具位姿使机床整机结构发生改变,进而导致机床振动特性发生演变[6]。同时,与转速相关的主轴系统动力学特性直接影响机床切削稳定性[7-8],因此,研究广义动态加工空间的机床切削稳定性,对于切削现场加工应用,保证零件加工质量,充分发挥机床效率至关重要。……