一种等离子切割钢管坡口机构的技术研究
2021-11-02赵艳红
赵艳红
摘 要:针对管-管对接焊接前的坡口加工技术,文章采用一种等离子切割钢管坡口的机构进行切割试验。综合分析,经过实际的切割试验,在等离子气工作压力为0.26MPa,割嘴距离钢管表面2~3mm,切割电流75~80A,针对∮30~106mm、壁厚2.8~6mm的钢管,以10~10.60 mm/s的切割速度进行切割,可以得到符合职业院校焊接技术应用专业实训教学需求的钢管坡口。
关键词:等离子切割;坡口机构;技术研究
中图分类号:TG483 文献标识码:A 文章编号:1001-5922(2021)10-0140-04
Research on the Technology of Plasma Cutting Steel Pipe Groove Mechanism
Zhao Yanhong
(Urumqi Technical College, Urumqi 830026, China)
Abstract:Aiming at the groove processing technology before pipe pipe butt welding, In this paper, a mechanism of plasma cutting steel pipe groove is used for cutting experiment. Comprehensive analysis, after the actual cutting test, when the working pressure of plasma gas is 0.26MPa, the distance between cutting nozzle and steel pipe surface is 2~3mm, the cutting current is 75~80a, for steel pipes of ∮30~06mm and wall thickness of 2.8~6 mm, cutting at a cutting speed of 10~10.60mm/s can obtain steel pipe grooves that meet the requirements of professional training and teaching of welding technology application in vocational colleges.
Key words:plasma cutting; groove mechanism; technical study
0 序言
職业院校焊接技术应用专业在技能训练实际操作过程中,为了节约试件的(钢板和钢管)用量,都是进行重复使用,具体做法是将焊后的试件沿焊缝边缘处切割开后再次进行坡口加工、组对、焊接练习,从而可以大大降低教学成本。
在管-管对接焊接的实训教学工作中,钢管的坡口加工是一个必不可少的重要环节。现阶段,对于焊后的管焊缝,职业院校大都使用普通车床进行钢管坡口的加工,传统的车加工技术,需要在车加工前,先用无齿锯将焊后的钢管沿焊缝边缘处切开,然后再用普通车床进行坡口加工,这种方法不仅加工工序多,而且加工效率较为低下,如果用无齿锯切割后的钢管端面成斜面、不垂直,还会增加车加工的难度,更加影响加工效率。
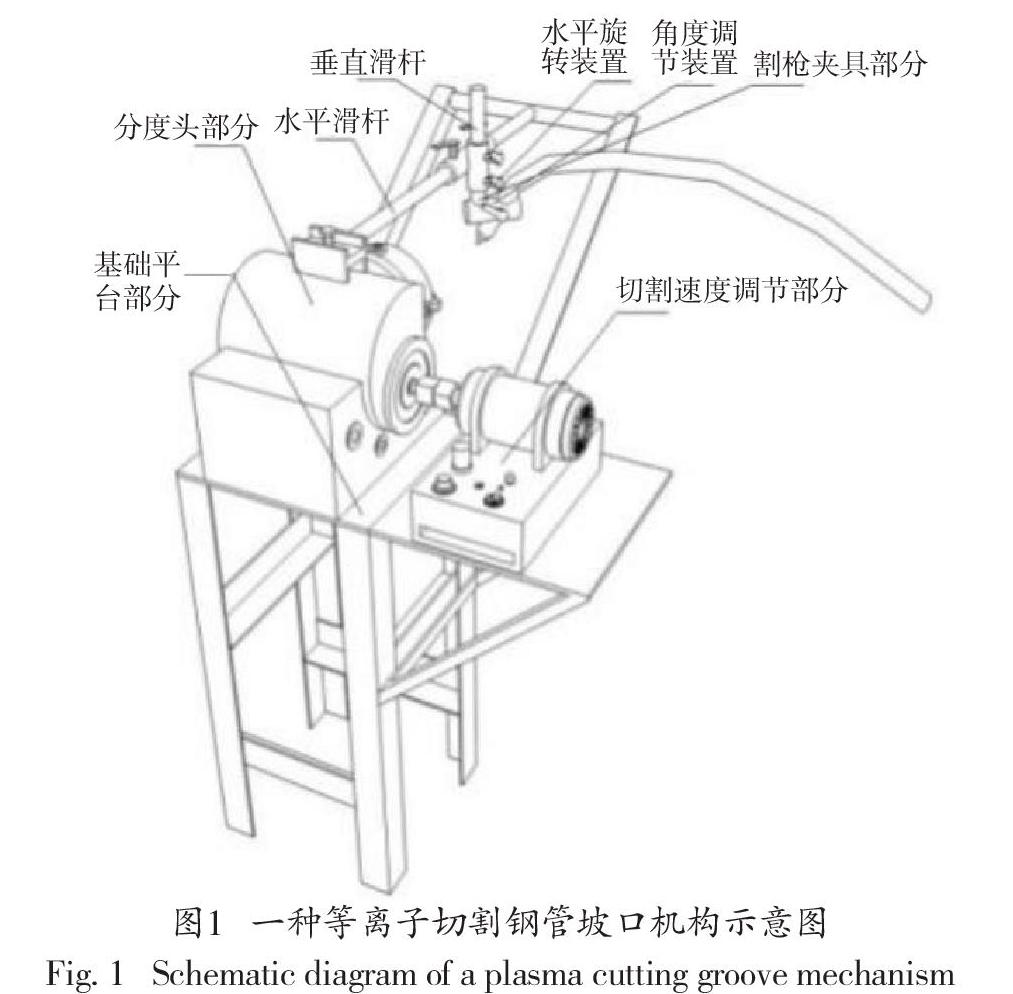
针对职业院校焊接技术应用专业实训教学中,管-管对接焊接项目钢管的坡口加工,文章对制作一种等离子切割钢管坡口机构的技术研发与实践进行研究,为一种等离子切割钢管坡口机构切割材质为Q235、直径为∮30~160mm的钢管坡口提供一定的切割基础数据,对扩大钢管坡口加工领域会起到促进作用。……
