回火时间对SA738Gr.B钢埋弧焊熔敷金属组织与性能的影响
2021-09-13张庆素冯伟胡晓波徐锴陈波
张庆素 冯伟 胡晓波 徐锴 陈波
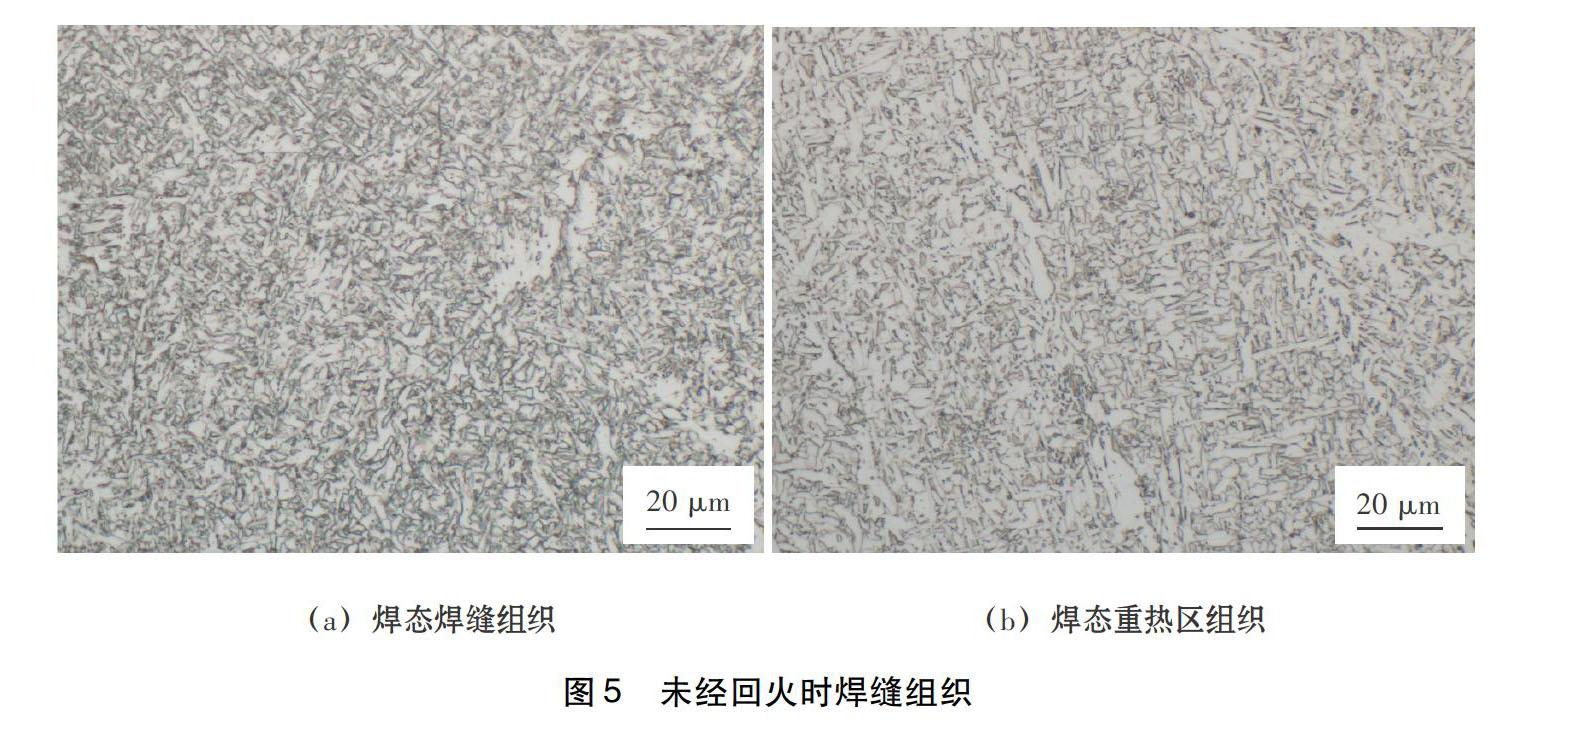
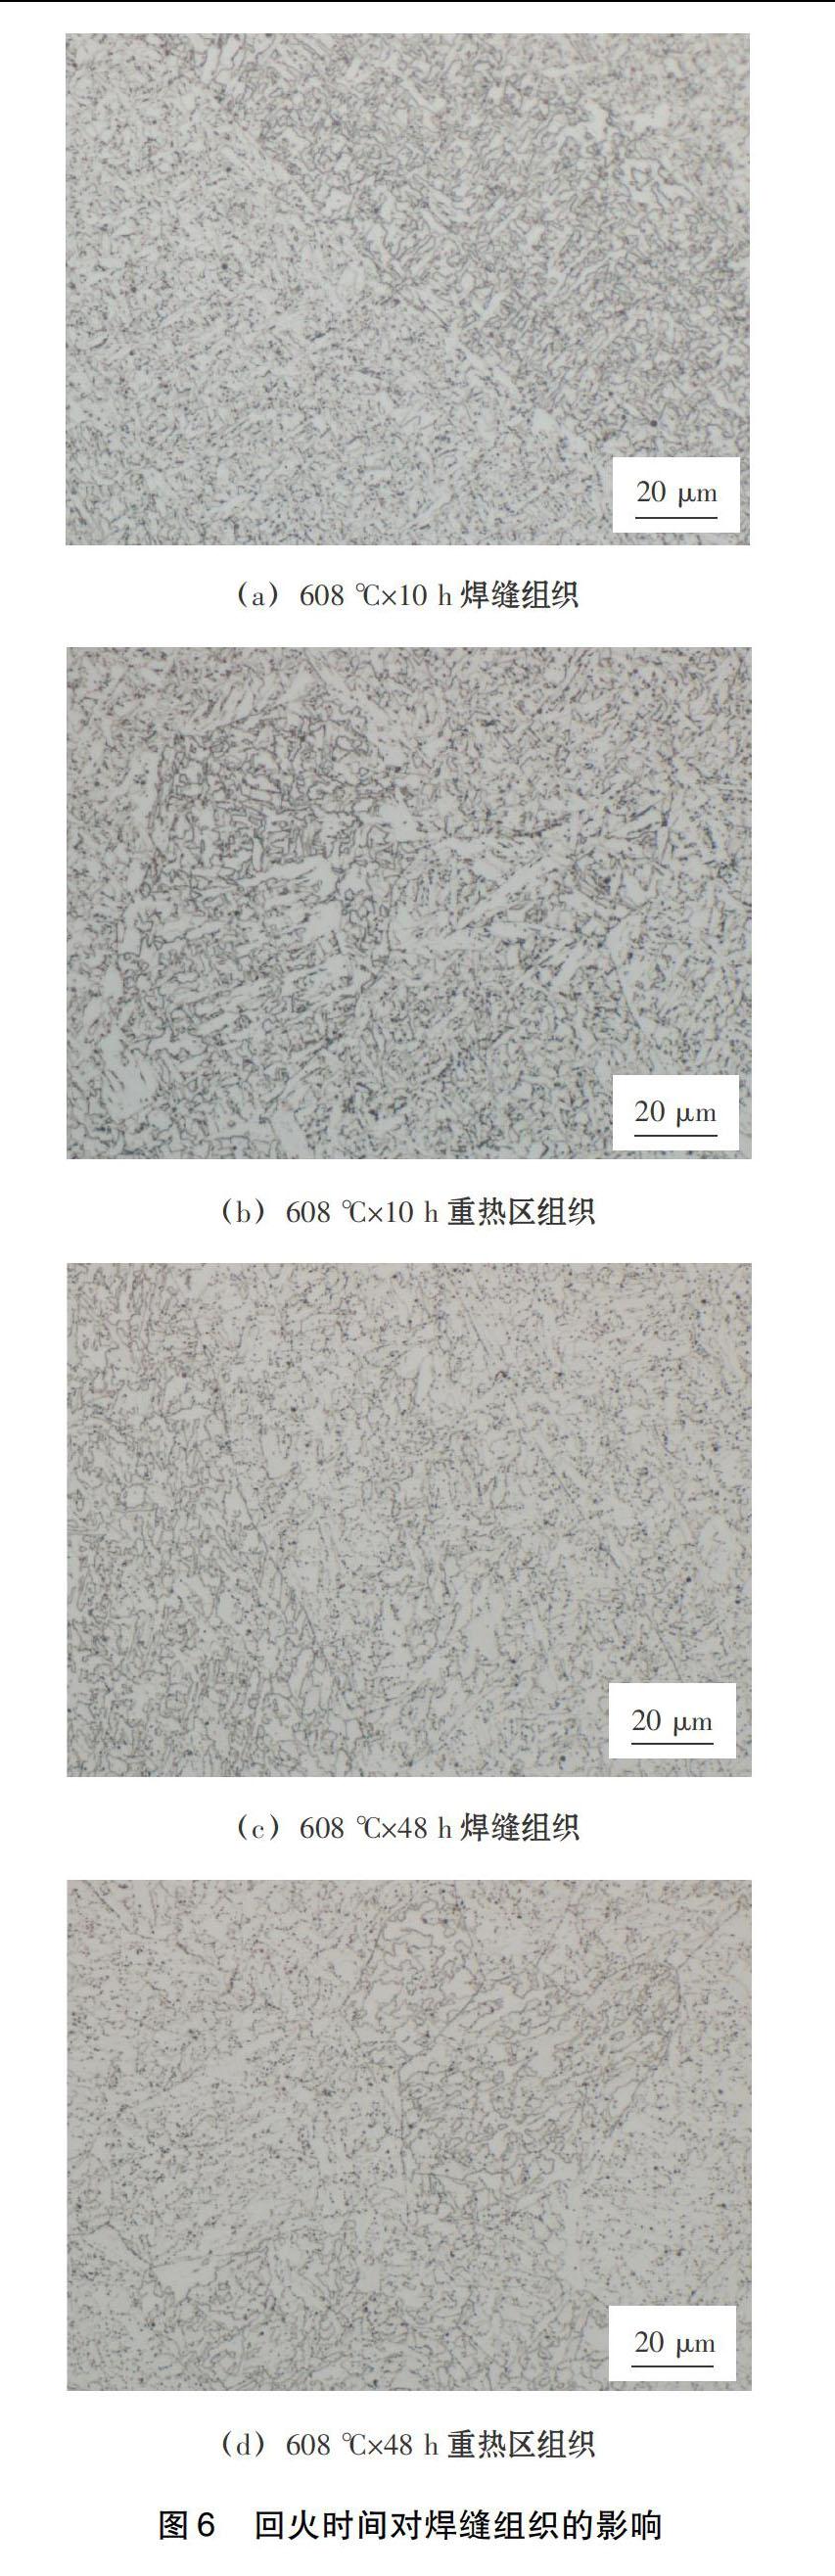
摘要: 文中研究了回火时间对SA738Gr.B钢埋弧焊熔敷金属性能的影响。结果表明,随回火时间延长,熔敷金属的强度和硬度逐渐下降,冲击温度≤-50 ℃,冲击韧性下降,冲击温度≥-30 ℃,该趋势不明显。熔敷金属韧脆转变温度在-30~-50 ℃区间。回火使焊缝及重热区的组织由低碳贝氏体向回火索氏体转变。铁素体发生回复再结晶,形态由针状转变成等轴晶。碳化物由片状转变成点状,分布于铁素体之上。
关键词: 埋弧焊; 熔敷金属; 回火时间; SA738Gr.B钢
中图分类号: TG 406
Effect of tempering time on microstructure and properties of deposited metal on SA738Gr. B steel by submerged arc welding
Zhang Qingsu1, Feng Wei1, Hu Xiaobo1, Xu Kai2, Chen Bo1
(1.Harbin Well Welding Co., Ltd., Harbin 150028, Heilongjiang, China;2.Harbin Welding Institute Limited Company, Harbin 150028, Heilongjiang, China)
Abstract: In this paper, the effect of tempering time on the performance of deposited metal on SA738Gr.B steel by submerged arc welding(SAW) was studied. The results showed that with the extension of tempering time, the strength and hardness of the deposited metal gradually decreased, when the impact temperature ≤-50 ℃, the impact toughness decreased, and the impact temperature ≥-30 ℃, the trend was not obvious. The ductile and brittle transition temperature of the deposited metal ranged from -30 ℃ to -50 ℃.The microstructure of weld and reheat zone changed from low carbon bainite to tempered sorbite. Ferrite restored to recrystallization and its morphology changed from acicular to equiaxed crystal. The carbide changed from flake to speck and distributed over the ferrite.
Key words: submerged arc welding; deposited metal; temper holding time; SA738Gr.B steel
0 前言
SA738Gr.B低合金鋼力学性能优良,可用于制作AP-1000和CAP1400核反应堆的安全壳[1-2]。其壳体的连接通常用埋弧焊进行。而焊缝在焊后需回火以消除应力并提高其塑韧性。温度和时间是影响回火组织的关键。长期以来人们往往只注重温度的影响,而对回火时间的影响缺乏研究。安全壳焊缝的回火温度通常为595~620 ℃[3-4],文中在前人研究的基础上,进一步研究了608 ℃下,回火时间对焊缝性能的影响。
1 试验方法
1.1 试验材料
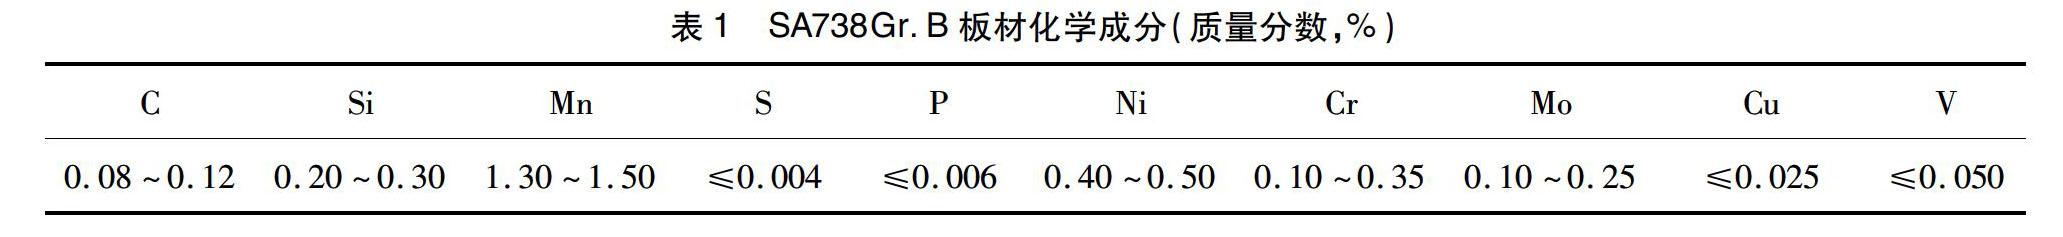
埋弧焊试验所用母材为SA738Gr.B板材,其化学成分及力学性能见表1、表2。所用焊材为哈尔滨威尔焊接有限责任公司研制的Mn-Ni-Mo低合金钢焊丝,牌号为H09MnNiMoHR,化学成分见表3,规格为4.0 mm;焊剂牌号为SJ18HR,与H09MnNiMoHR焊丝匹配。焊剂规格为0.25~1.70 mm,符合AWS A-5.23 F8P3-EF3-F3要求,同时满足NB/T 47018—2017和GB/T 5293—2018的要求。
1.2 试验方法
按GB/T 5293—2018制备试件。室温拉伸按GB/T 228.1—2010和GB/T 2652—2008进行,冲击试验按GB/T 229—2007进行,硬度测试按GB/T 231.1—2018进行。焊接电源为LINCOLN AC/DC-1000。埋弧焊工艺参数见表4。
通过对比熔敷金属在608 ℃×0 h,608 ℃×10 h,608 ℃×24 h,608 ℃×40 h和608 ℃×48 h回火后的组织性能,分析了回火时间对其影响。……