基于非熔化极惰性气体保护电弧焊的铝合金车身维修研究
2021-03-28张影
张影
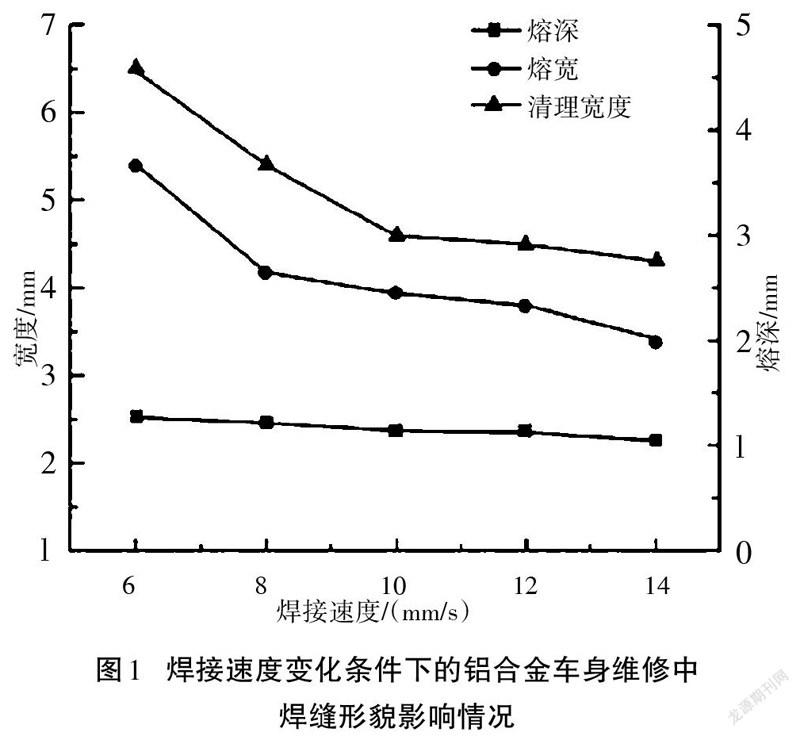
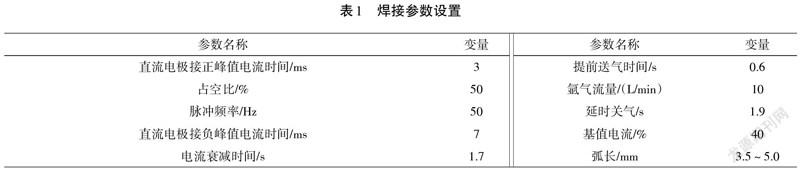
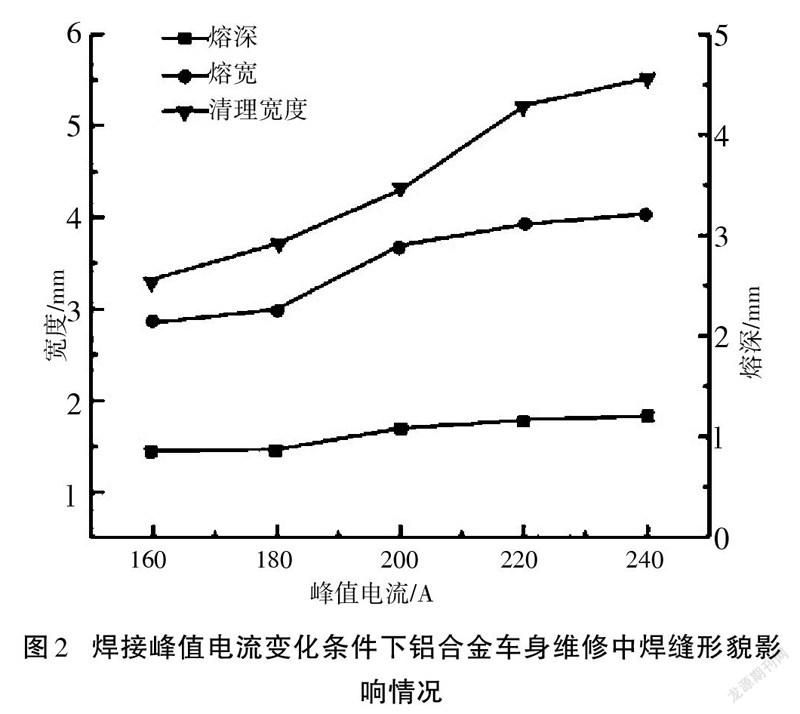
摘 要:基于提高铝合金车身维修水平的目的,从焊接工艺视角出发,提出将非熔化极惰性气体保护电弧(Tungsten Inert Gas,TIG)焊应用于铝合金车身维修,着重分析非熔化极惰性气体保护电弧焊工艺中焊接速度和焊接峰值电流对焊缝形貌的影响。结果表明:车身焊缝熔深受焊接速度的影响较小,熔宽和清理宽度受此影响较大;熔深受峰值电流变化的影响较小,熔宽和清理宽度受此影响较大。建议车身维修期间,设定TIG焊接速度为10~12 mm/s,峰值电流为180~200 A。另外,针对TIG焊接在铝合金车身维修中的应用给出了一些指导性建议。
关键词:非熔化极惰性气体保护电弧焊;车身维修;铝合金
中图分类号:TG445 文献标识码:A 文章编号:1003-5168(2021)32-0041-03
Research on Aluminum Alloy Body Maintenance Based on TIG Welding
ZHANG Ying
(Huai'an Bioengineering Vocational College, Huai'an Jiangsu 223000)
Abstract: In order to improve the maintenance level of aluminum alloy body, from the perspective of welding process, this paper proposes to apply non consumable inert gas arc welding to aluminum alloy body maintenance, and focuses on the effects of welding speed and welding peak current on weld morphology in non consumable inert gas arc welding process. The results show that the welding speed has little effect on the weld fusion width of vehicle body, and the fusion width and cleaning width are greatly affected by this; The melting width and cleaning width are greatly affected by the change of peak current. It is recommended to set the TIG welding speed as 10~12 mm /s and the peak current as 180~200 A during body maintenance. this paper gives some guiding suggestions for the application of TIG welding in aluminum alloy body maintenance.
Keywords: tungsten inert gas welding;body maintenance;aluminium alloy
铝合金具有导热导电性能强、材料密度较小、强度高以及耐腐蚀性好的优势,可满足车身加工需求,因而在车辆生产中应用比较广泛[1]。随着我国经济水平的不断提升,汽车行业发展速度不断加快[2],道路车辆数量逐渐增加,导致交通安全事故时有发生。铝合金车身维修作为交通事故车辆维修的主要内容之一,对焊接技术水平的要求较高[3]。传统焊接工艺在焊缝形貌把控方面有待改进[4]。为此,本文提出运用非熔化极惰性气体保护电弧(Tungsten Inert Gas,TIG)焊技术,采用试验分析的方式,探究该技术在铝合金车身维修中的应用。
1 试验设备与材料
1.1 试验设备
本次试验搭建铝合金车身焊接信息采集与控制系统,并将其作为TIG焊接技术应用中焊缝形貌把控的依据。试验期间使用到的设备包括焊接子系统、中心控制计算机、送丝子系统、固高端子板、图像采集子系统和运动控制子系统。……