海工用X100管线钢管的焊接工艺及接头质量分析
2020-04-20冯胜昆周文张徐强屈江艳
冯胜昆 周文 张徐强 屈江艳
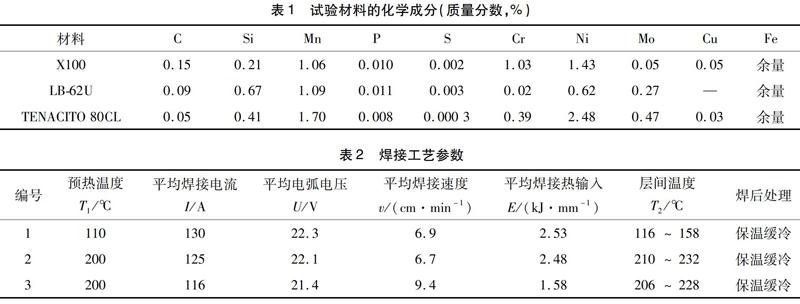
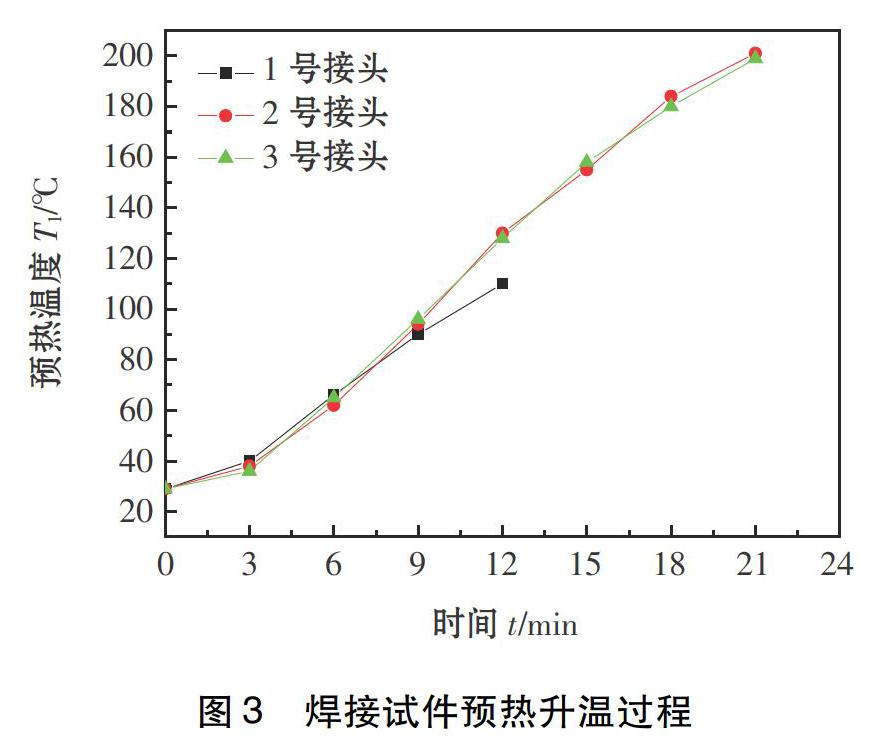
摘要:采用海洋平台建造中符合AWS D1.1标准的6GR位置特定坡口形式,利用焊条电弧焊(SMAW)单面焊双面成形工艺焊接某国产X100管线钢管。通过拉伸、冲击、弯曲试验检测接头的力学性能,通过光学显微镜对比分析X100管线钢焊接接头坡口两侧熔合线显微组织。结果表明,该公司生产上所用的X100管线钢管在6GR位置通过合适的预热及焊接热输入可以得到满足结构使用性能要求的焊接接头,但接头未开坡口侧在-40 ℃冲击时,冲击吸收能量相对较低,原因是未开坡口侧(直边)熔合线晶粒粗化严重,大晶粒晶界有相互连接趋势。
关键词:X100管线钢管;6GR位置;预热;未开坡口侧;晶界
中图分类号:TG 442
Abstract:Singleside welding by shielded metal arc welding with the inevitable 6GR position and specific groove form (comply with AWS D1.1)in the offshore platform construction was used to weld domestic X100 pipeline steel pipe. The mechanical properties of the welded joints were measured by tensile strength, impact toughenss, bending test and the microstructures of the fusing area on both sides of the X100 pipeline steel welded joint were analyzed by optical microscope. The results shown that the X100 pipeline steel pipe used in the production of the company could be welded and the weld joint could satisfy the structural performance requirement with appropriate preheating and welding heat input control in the 6GR position. But the impact absorbed energy was relatively low on the unbevel side of the welded joint in the -40 ℃ impact test. The reason is that the grain size coarsened severely and the boundary of the large grains have a mutual connection trend in the fusion area of the unbevel side (square side).
Key words:X100 pipeline steel pipe;6GR position;preheating;unbevel side;grain boundary
0 前言
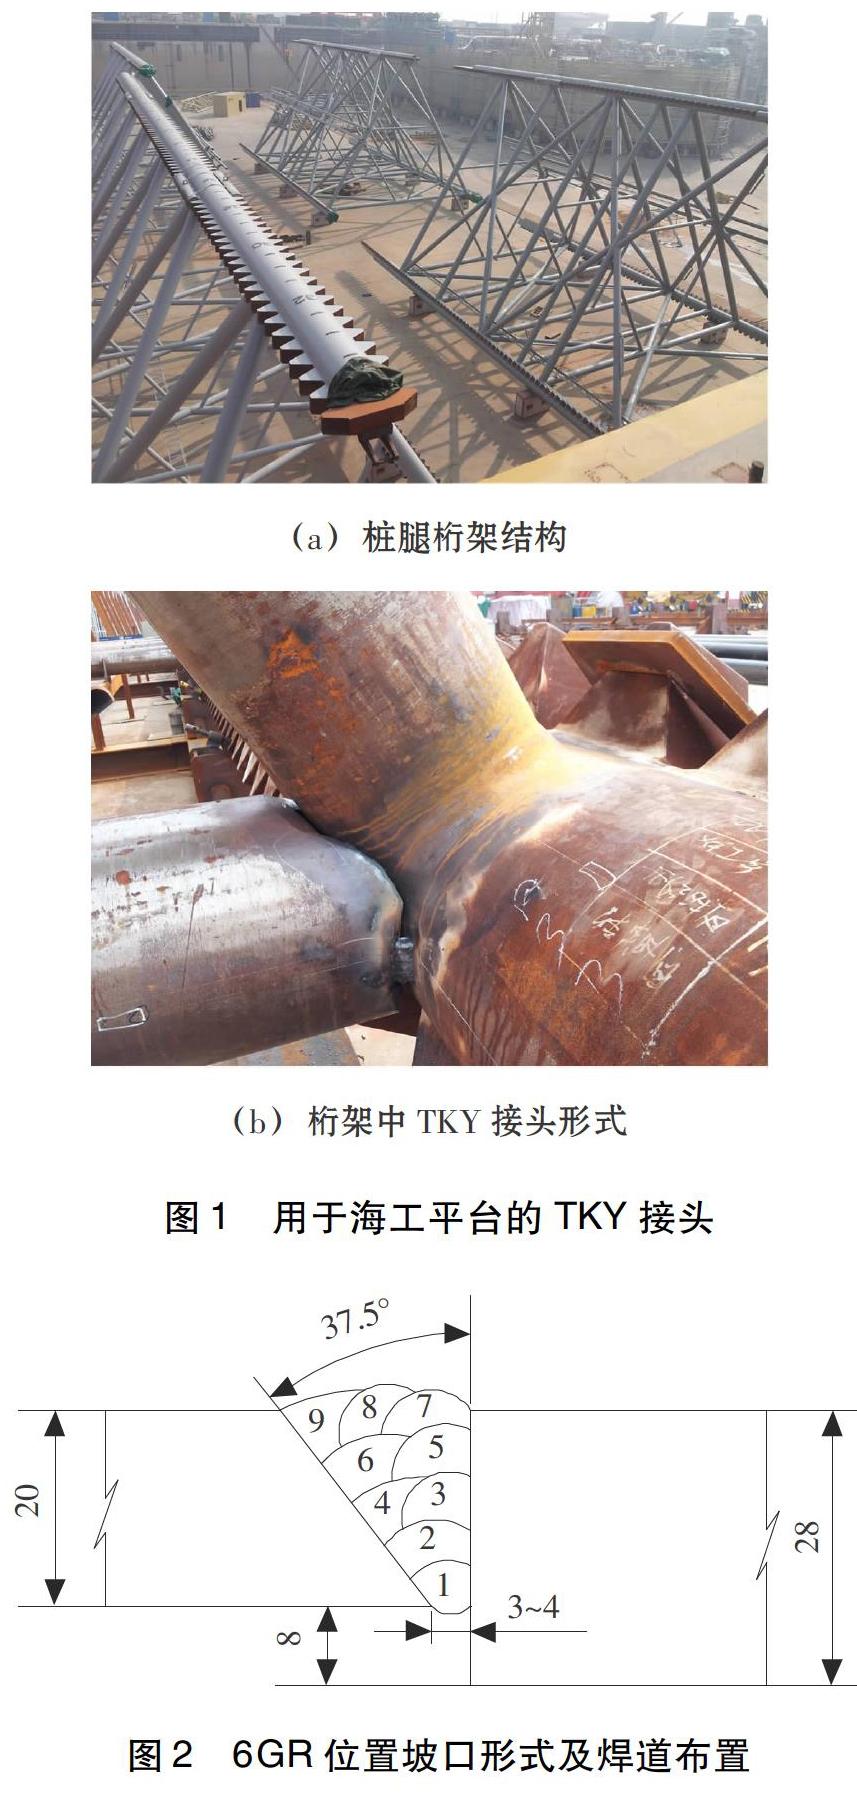
在海洋平臺制造中,为满足减轻结构重量及低温力学性能要求,桩腿桁架结构用690 MPa级低温高强钢管已得到广泛应用,但此类高端材料,如Oceanfit 690,EQ70管等一直主要由国外进口[1]。受国际经济形势以及高昂的进口材料费用的影响,建造海洋平台的利润空间已逐渐降低,目前,国内主要海洋平台制造厂已逐渐开展利用X100管线钢管代替进口材料,基于国内石油运输用X100管线钢管的开发应用已有相当基础[2],且生产成本相对较低,国内已有厂家开发出供海洋平台桁架用的低温X100管线钢管,且已实现小部分焊接生产应用[3-4]。
海洋平台桁架结构用X100管线钢管不同于传统石油、天燃气运输用X100管线钢管,传统石油运输用X100管线钢管主要受内部流体压力作用,且服役温度一般……
