W4Mo3Cr4VSi钢喷油泵柱塞热处理质量的控制
2021-10-20李振华
李振华


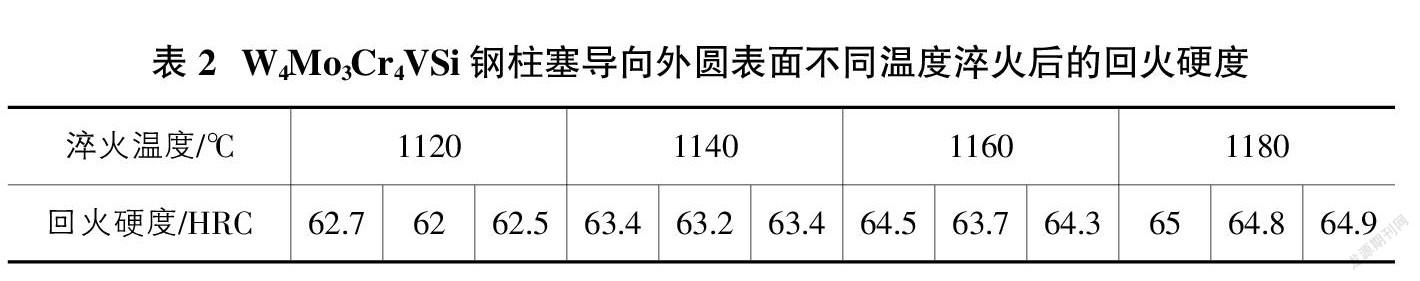
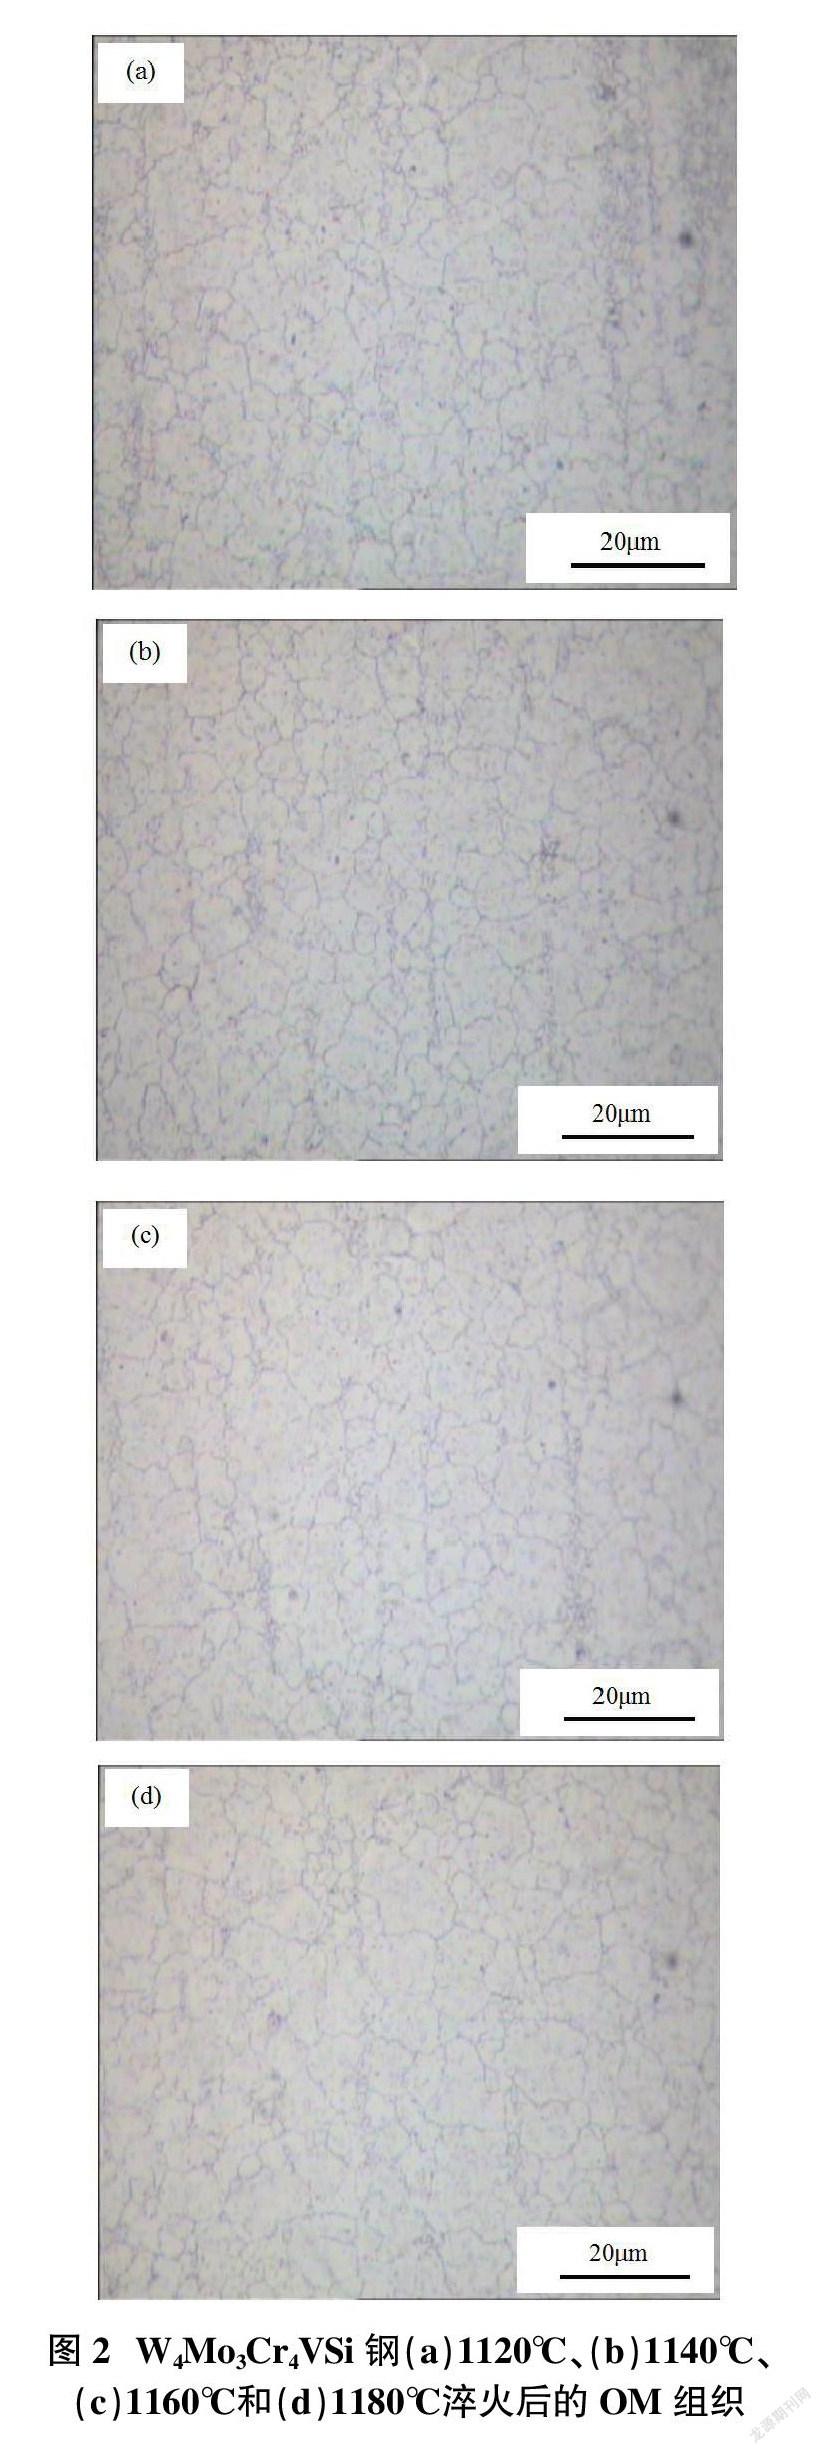


摘要:本文从金相组织、TiN镀层和热处理变形等方面对W4Mo3Cr4VSi钢柱塞的质量进行试验研究、观察和测量。试验结果表明:W4Mo3Cr4VSi钢柱塞的最佳淬火温度为1140~1160℃,淬火晶粒度10~10.5级。TiN镀层的表面硬度达2400HV1,镀层与基体的结合强度级别为HF-2。淬火油的状态、淬火入油方式、油淬时间均影响柱塞的淬火变形,采用轴向垂直入静油淬冷1.5min可将柱塞的径向变形量控制在0.4mm以内。柱塞热处理后的轴向平均伸长量为0.474mm,但散差达0.28mm。
Abstract: In this paper, the quality of W4Mo3Cr4VSi steel plunger was studied, observed and measured from the aspects of metallographic structure, TiN coating and heat treatment deformation. The results show that the optimum quenching temperature of W4Mo3Cr4VSi steel plunger is 1140~1160℃ and the quenched grain size is 10~10.5. The surface hardness of TiN coating is 2400HV1, and the bonding strength of TiN coating and substrate is HF-2. The quenching deformation of the plunger is affected by the state of the quenching oil, the injection mode of the quenching oil and the quenching time. The radial deformation of the plunger can be controlled within 0.4mm by using the axial vertical injection of the static oil for 1.5min. After heat treatment, the average axial elongation of the plunger is 0.474mm, but the dispersion is 0.28mm.
关键词:W4Mo3Cr4VSi钢;柱塞;TiN镀层;淬火变形
Key words: W4Mo3Cr4VSi steel;plunger;TiN plating;quenching distortion
中图分类号:TG713 文献标识码:A 文章编号:1674-957X(2021)20-0138-04
0 引言
柱塞偶件是喷油泵中最精密的偶件之一,由柱塞和柱塞套组成。其工作原理为凸轮通过顶杆驱动柱塞在柱塞套内往复运动,完成喷油泵吸油和泵油的过程,其作用除了要使燃油增压,还要精确地控制供油量和喷射时间。柱塞偶件的质量对燃油喷射系统各工况的供油均匀性、喷油泵泵端喷射压力、系统的可靠性以及柴油机燃油工作过程和性能指标有很大的影响,直接影响到柴油机的正常工作和可靠性[1]。当前油机主要向低速大功率方向发展,为满足柱塞在高频、高压及一定环境溫度下工作的要求,柱塞必须具有高硬度、高耐磨性以及较好的尺寸稳定性和较高的接触疲劳强度,这对柱塞选材及热处理提出了较高的要求。
本文针对某型号柴油机喷油泵柱塞的热处理质量从金相组织、TiN镀层和热处理变形等方面进行了研究。
1 试验材料和方法
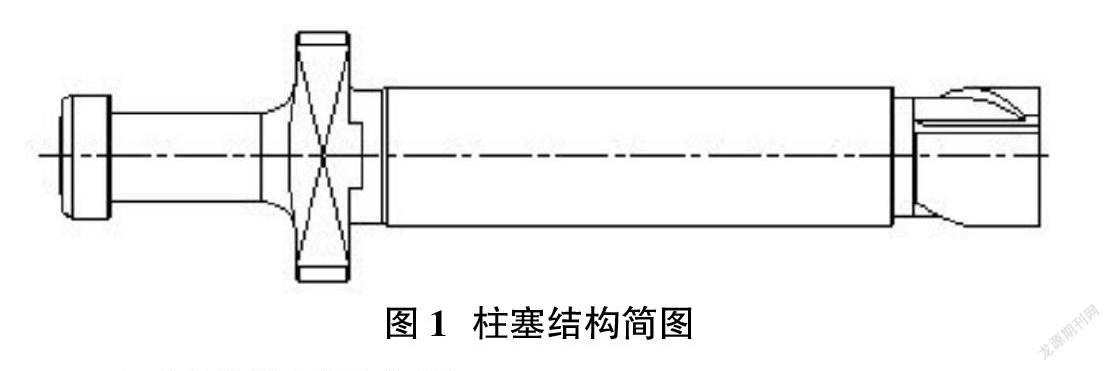
试验用W4Mo3Cr4VSi钢圆棒料,机加工成ф31×220mm的某种型号的柱塞,柱塞结构简图如图1所示。……