超长换热器管束的制造工艺
2016-05-30李发林刘利和
李发林 刘利和
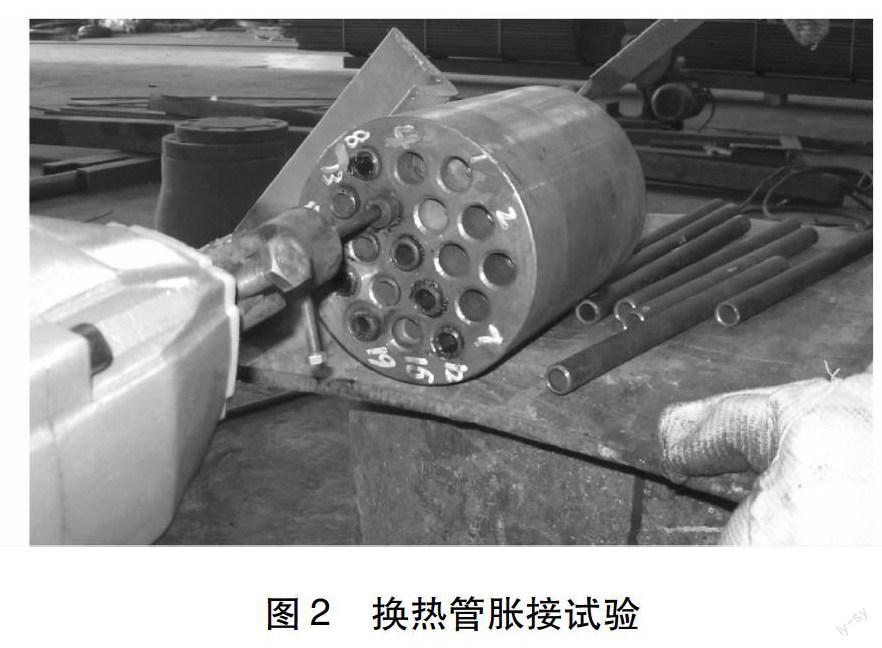
摘要: 主要介绍了合成塔进出口换热器超长管束装配、吊装和胀接等制造工艺,重点阐述了该换热器装配、吊装的特殊辅助工装,通过胀接试验确定具体的胀接工艺,合理装配导流筒,顺利完成超长管束的装配和整体水压试验。
关键词: 管束装配;吊装;胀接工艺;导流筒
中图分类号: TG421
Abstract: This article mainly introduces the assembly hoisting and expanding method of the import and export heat exchanger of synthetic tower. The special auxiliary tooling of assembly and hoisting that are used in the exchangers manufacturing process were mainly expounded. The specific expanding process were determined experimentally. Then, the assembly of ultra long tube bundle and hydrostatic testing were successfully complete based on the rational use of guide cylinder.
Key words: assemble of tube bundle; hoisting; expanding process; guide cylinder
0 前言
某煤化工项目中的合成塔进出口换热器,外形尺寸1 600 mm/1 300 mm×110 mm/80 mm×21 692 mm,净重120.167 t,筒体材料14Cr1MoR厚度80 mm,100 mm及110 mm;管板材料14Cr1MoⅣ,厚度150 mm;换热管材料15CrMo,规格14 mm×2 mm×18 000 mm。
该产品由于管束太长、换热管规格较小、管束的重量达到50 t,给生产制造带来非常大的困难,其中制造中存在的难点主要有管束装配,管束起吊、穿入壳程筒体,需要制定合理的施工方案才能保证18 m长的管束顺利进入筒体。
1 换热器管束关键制造工艺
1.1 管束装配
将折流板上因钻孔产生的毛刺用手提砂轮机打磨去除,同时用砂轮机将折流板外圆两侧打磨成R2~3 mm圆角。管束总长18 m,装配时要充分考虑到穿管束的场地和管束进筒体的场地,保证装配穿管后的管束不得翻身、不得掉头。
穿管束前搭花架,固定管板装配拉杆,紧固拉杆螺母,中间折流板下面用特殊槽钢支撑,两侧折流板底下垫角钢与地面支撑,起支撑作用的两侧角钢之间用角钢连接。
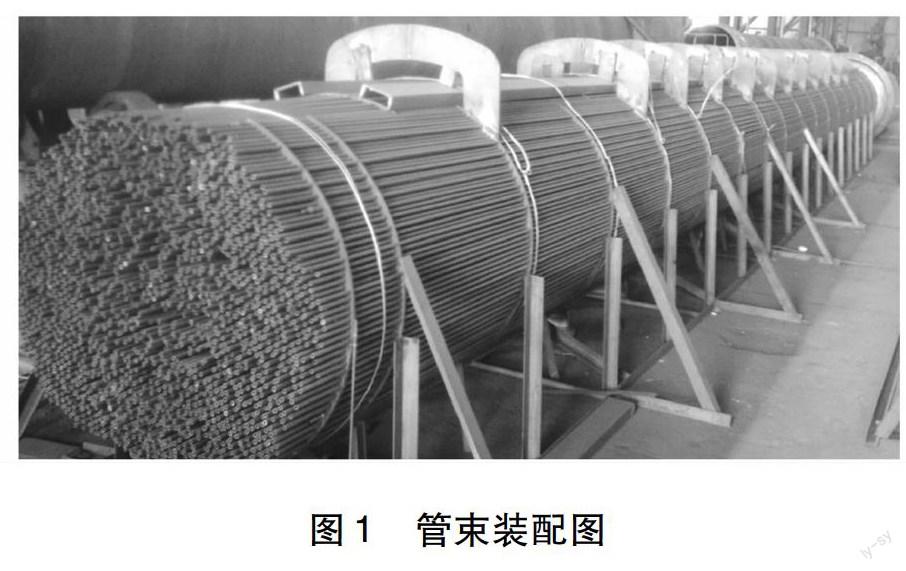
在两侧折流板层与层之间加筋板,筋板与折流板之间采用连续焊。如图1所示。利用行车勾住横梁吊装工装吊起整个管束,在管束底部加支撑,焊接中间折流板下部的滑道,在焊接滑道的过程中行车上的起吊工装仍需处于稳定状态。……