对焊铣刀断裂原因分析
2021-07-20王春奕朱蒨欧红燕张全新
王春奕 朱蒨 欧红燕 张全新
摘要: 文中通过对断裂的对焊铣刀各部位进行化学成分、硬度、金相组织的检测分析,侧重从宏观和微观对铣刀各部位显微组织进行对比分析,结合铣刀的焊接和热处理过程,对铣刀断裂原因进行了分析讨论。结果表明,对焊铣刀在最终热处理时淬火加热区域超过焊缝部位,使焊缝附近的高速钢热影响区产生很大的组织应力和热应力,最终导致了对焊铣刀的断裂。
关键词: 对焊铣刀; 淬火; 热影响区; 组织应力; 热应力
中图分类号: TG 47
Fracture analysis of butt welding milling cuttre
Wang Chunyi1, Zhu Qian2, Ou Hongyan1, Zhang Quanxin1
(1.Chongqing Iron and Steel Research Institute Co.,Ltd.,Chongqing 400084,China;
2.Chongqing Industry Polytechnic College, Chongqing 401120, China)
Abstract: In this paper, the chemical composition, hardness and metallographic structure of the broken welding milling cutter were tested, and the microstructure of each part of the milling cutter was analyzed and compared from the macroscopic and microscopic aspects. Combined with the welding and heat treatment process of the milling cutter, the reasons for the fracture of the milling cutter were analyzed and discussed. The analysis results showed that the quenching heating area of butt welding milling cutter exceeded the weld area of the milling the cutter in the final heat treatment, which made the heat affected zone of high-speed tool steel near the welding seam produce great structural stress and thermal stress, which led to the fracture of the butt welding milling cutter.
Key words: butt welding milling cutter; quenching; heat affected zone; microstructure stress; thermal stress
0 前言
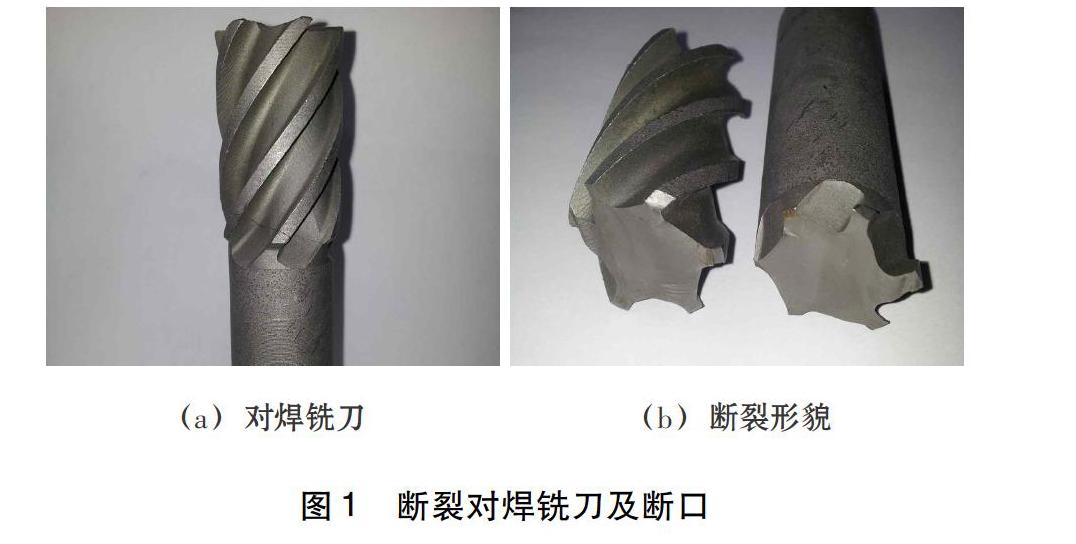
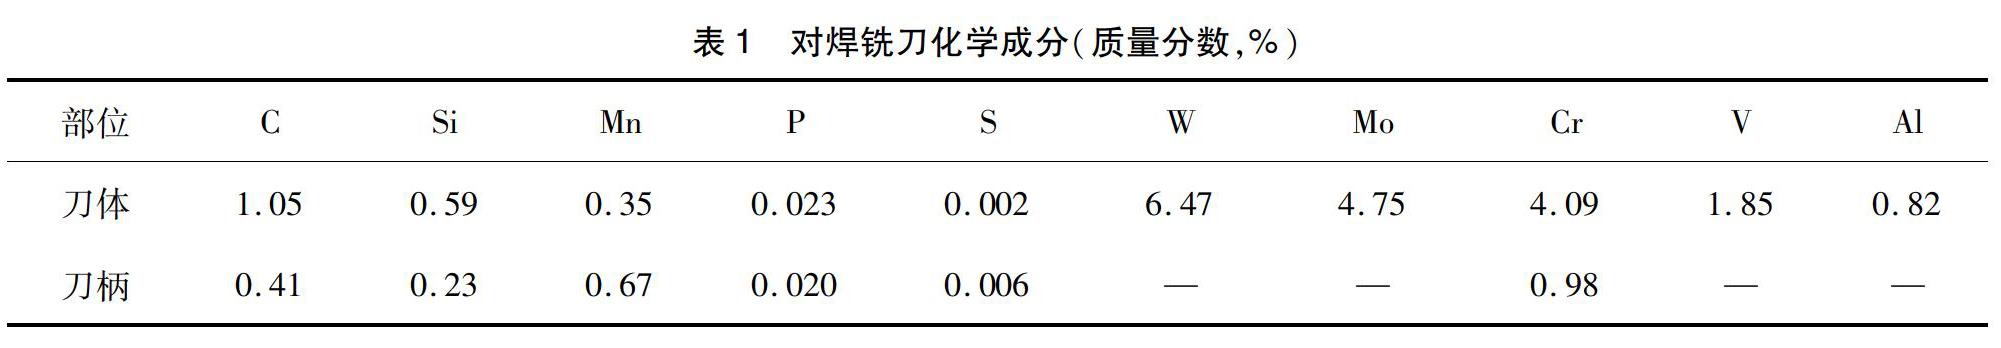
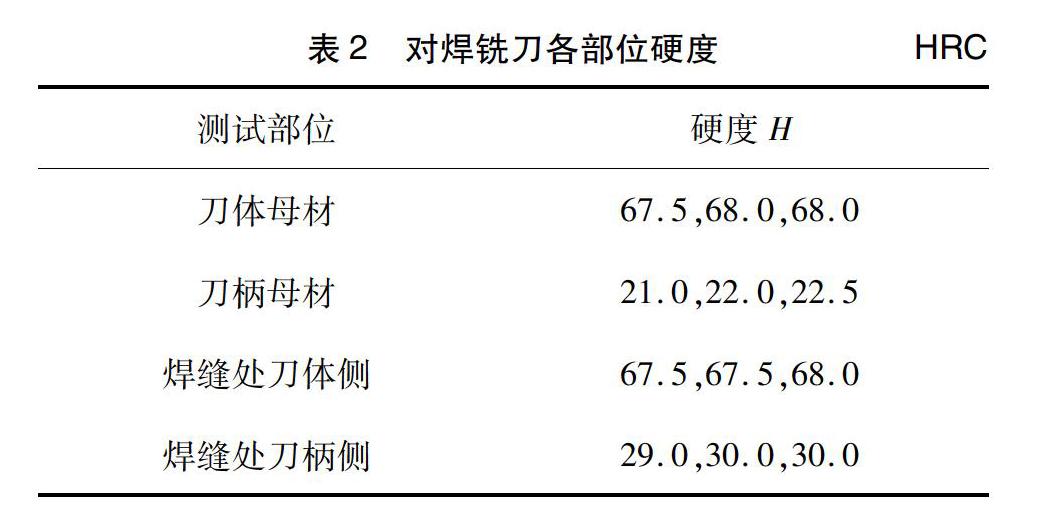
某公司生產的焊接带柄高速钢铣刀,通过结构钢与高速钢对焊而成,铣刀刀体材质为W6Mo5Cr4V2Al(M2Al钢),刀柄材质为40Cr钢,对焊铣刀在经过最终热处理后发生断裂,断裂部位位于离焊缝约5~10 mm处的刀体一侧,发生断裂的铣刀占有较大比例,给该公司造成了一定的经济损失。为防止产品再次出现此类问题,对断裂铣刀进行了化学成分分析、硬度检测、金相高低倍组织观察,以查找铣刀断裂的真正原因。1 试验设备文中使用德国SPECTRO LAB直读光谱仪及CS-206型红外碳硫分析仪进行化了学成分分析,使用HR-150A型洛氏硬度计进行了试样硬度检测,使用日本OLYMPUS GX71型光学显微镜进行了金相组织观察。2 理化检验2.1 化学成分分析断裂对焊铣刀及断口形貌如图1所示,对铣刀刀体和刀柄试样分别进行了化学成分分析,结果见表1。2.2 硬度检测对铣刀刀体和刀柄试样的不同部位进行了硬度检测,结果见表2。2.3 金相检验如图2所示,将刀体母材和刀柄母材试样分别经预磨抛光并用4%硝酸酒精溶液侵蚀,放大100~500倍进行高倍观察,发现高速钢铣刀金相组织为回火马氏体+碳化物,如图2a所示。……