SA213-T91和12Cr1MoV异种钢焊接接头断裂分析与处理
2021-02-08赵飞俞科明王星辰胡丰丰
赵飞 俞科明 王星辰 胡丰丰
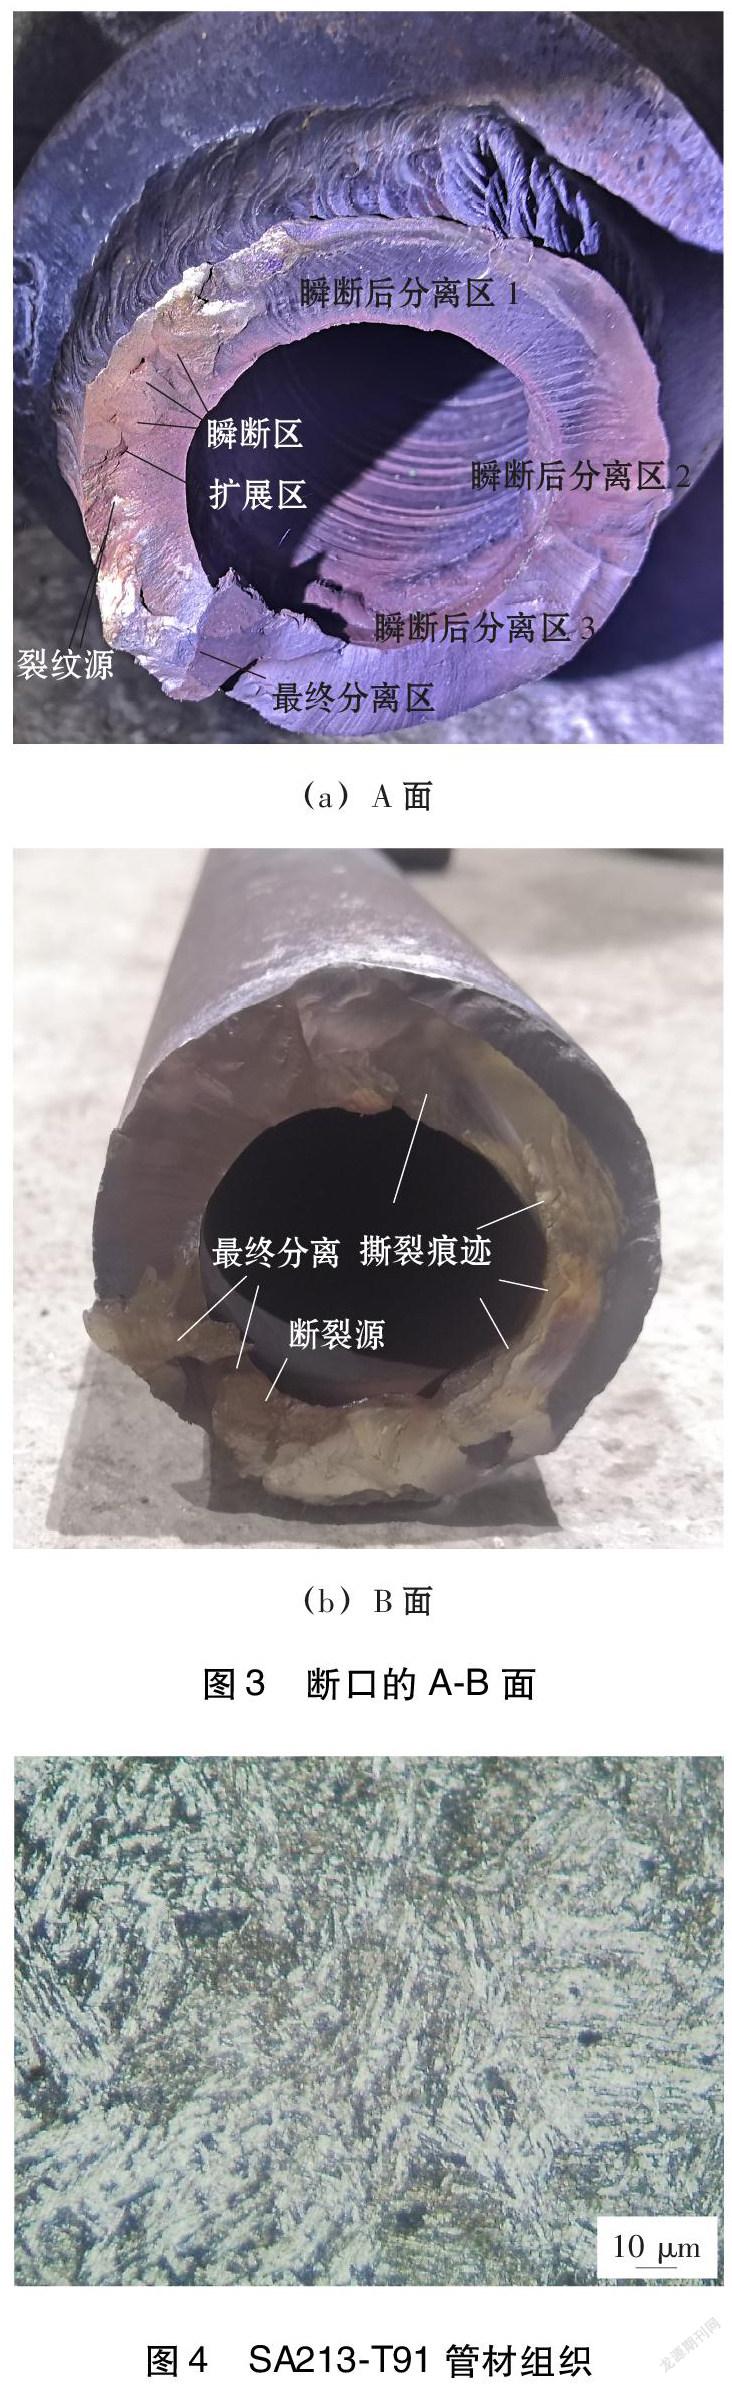
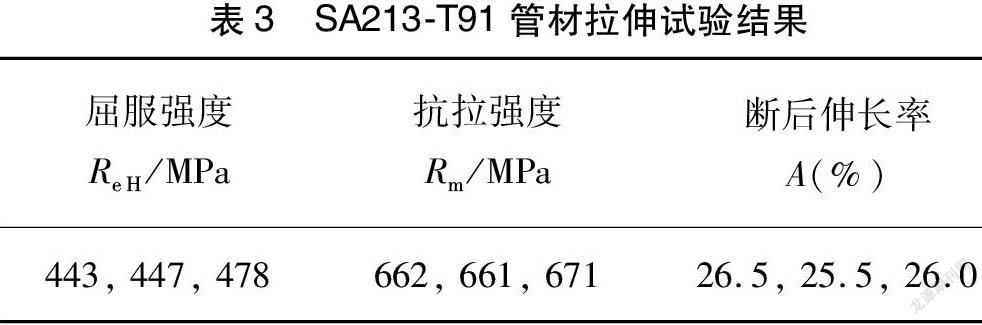
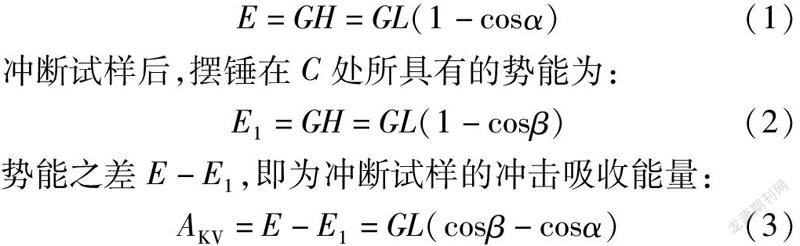
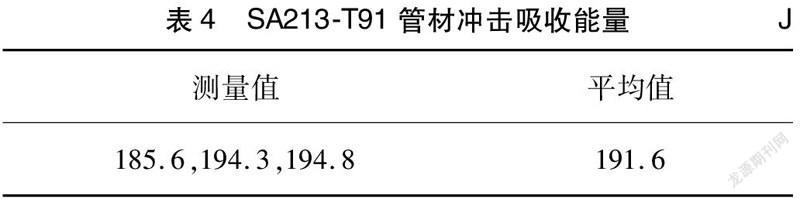
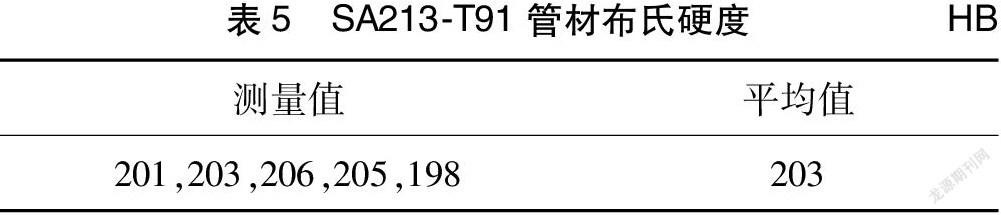
摘要:某电厂SA213-T91和12Cr1MoV异种钢焊接接头断裂后,通过对断口截面的观察、焊缝及断裂侧管材的金相检验、拉伸试验、冲击试验和硬度检验等方法分析断裂原因。研究结果表明,试样的强度、冲击韧性、硬度和金相组织符合要求,断裂的主要原因是焊接接头熔合线附近区域的裂纹在频繁的温度变化和压力变化的作用下迅速扩展生长,最终导致结构件断裂。最后对返工、焊接方法、焊接过程的控制及焊后热处理进行了介绍。
关键词:SA213-T91;12Cr1MoV;断裂;焊后热处理
中图分类号:TG 442
Abstract:After the fracture of SA213-T91 and 12Cr1MoV dissimilar steels welded joints in a power plant, fracture causes were analyzed through methods of the observation of fracture section, metallographic test of welds and pipes on the fracture side, tensile test, impact test and hardness test. The result showed that the strength, impact toughness, hardness and metallographic structure of the samples met the relative requirements, and the main reason of fracture was that the crack near the fusion line of welded joint expanded and grew rapidly under the action of frequent temperature and pressure changes, resulting in fracture. Finally, rework, welding method, control of welding process and post weld heat treatment were introduced.
Key words:SA213-T91;12Cr1MoV;fracture;residual stress;post weld heat treatment
0 前言
現阶段,碳达峰、碳中和摆在环资工作的突出位置,火力发电厂作为保证电力供应的主要力量,调峰压力与日俱增,为了能适应复杂多变的工况,要求火力发电厂设备稳定性更高,吹扫冲管是机组运行前的重要阶段,是保证设备稳定运行的必须步骤,冲管所使用的控制阀门及其阀门后管道一般为临时管道。
SA213-T91和12Cr1MoVG化学成分及理化性能差异较大,焊接时容易产生成分偏析或者出现其他焊接缺陷[1-3],导致难以获得高质量的焊接接头。因此在实际生产中,通常使用ER90S-B9类焊材或TIG-R40等过渡性材料,减少化学成分的偏析现象,以保证焊接质量的控制。
1 焊接工艺及热处理
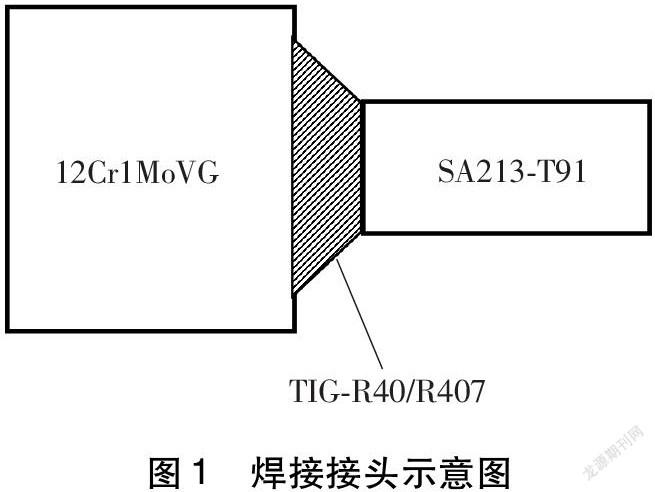
某电厂焊接接头规格48 mm×7 mm,材质为SA213-T91和12Cr1MoVG异种钢对接,阀门侧12Cr1MoVG,管子侧SA213-T91,焊材选用TIG-R40/R407,焊接方式GTAW+SMAW,两侧管材已经历十余台机组冲管任务,工况为反复加热,压力反复变化。焊接接头示意图如图1所示。
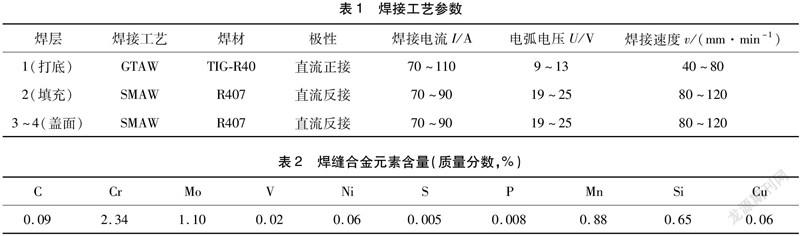
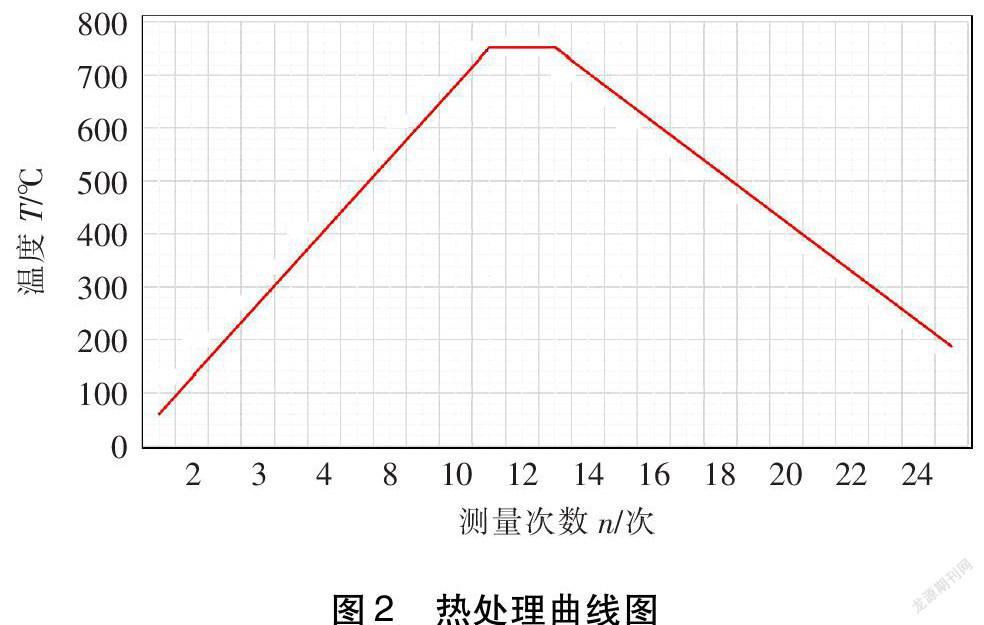
焊接工艺焊接方式为钨极氩弧焊+焊条电弧焊(GTAW+SMAW),焊材选用TIG-R40和R407,焊接位置6G。……