整体桥架自动冲压生产线控制系统调试中存在的问题研究
2018-07-13原保忠王玉玲
原保忠 王玉玲
摘 要:在一条冲压生产线上生产整体桥架的一个产品系列,要同时满足不同腰高的连接孔、梯式桥架横担冲孔、拉伸及托盘式桥架底部环形筋的拉伸加工。前期伺服送料机按送料长度值等于桥架长度值的控制方式进行步距送进生产,经过两次大的程序控制调整,都未能保证桥架长度尺寸和腰部连接孔位置尺寸的精度;最终伺服送料机以单步距分两次进给,每送完一个步距就清零一次,既保证了前后两台设备冲压动作在桥架的位置误差,也保证了桥架总长尺寸公差。
关键词:整体电缆桥架;自动冲压线;控制程序;桥架长度误差;连接孔位置尺寸
中图分类号:TM925.52;TP278 文献标识码:A 文章编号:1003-5168(2018)16-0070-03
Analysis of the Problems Existing in the Debugging of the Control System
for the Automatic Stamping Production Line of the Integral Bridge Frame
YUAN Baozhong WANG Yuling
Abstract: In a stamping production line, a series of integral bridges will be produced, which should simultaneously meet the tension of the connecting holes of different waist height, the punching of the ladder type bridge, the drawing of the bottom ring of the bottom of the tray type bridge. According to the control mode of the length value equal to the length value of the bridge, the prophase servo feeder could be sent to the production by step distance. After two large program control adjustment, the length of the bridge was not guaranteed and the precision of the location size of the connecting hole of the waist was not guaranteed. The final servo feeder was divided into two times with one step distance, and every step was cleared once, which ensured the position error of the stamping action of the two equipment in the bridge frame, and also ensured the length tolerance of the bridge.
Keywords: integral cable bridge;automatic stamping line;control program;bridge length error; connection hole location size
為了满足AP1000(核电标准)的高抗震要求,许昌美特桥架股份有限公司研发了一种整体高抗震桥架。为生产此桥架,公司定制了全套生产线。而冲压生产线是整条生产线的一部分,要求其满足整体桥架系列产品生产,方便品种更换和调试。也就说,要满足不同腰高的连接孔和梯式桥架横担冲孔、拉伸和及孔托盘桥架底部环形筋的拉伸的加工;通过生产线调试,完善控制程序,优化生产流程。
1 桥架的结构
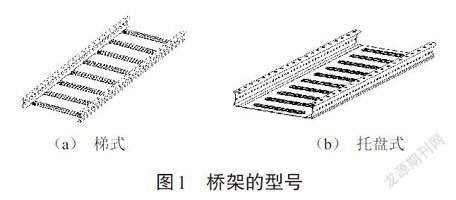
许昌美特桥架股份有限公司研发的高抗震桥架,型号有梯式和托盘式,见图1。
桥架参数:宽度W=300/400/500/600mm,腰高H=70/90/100mm,材料厚度t=2mm,桥架长度L=2 000/3 000mm。
桥架产品的结构特点为:桥架两侧腰上中心线处各有一排连续Φ9mm×20连接孔,上部各有一排盖板孔Φ10mm×35;梯式桥架底部是横担,横担中心线上有一排Φ7mm×25孔,每个横担中心距是250mm:两侧盖板孔中心与横担中心对应,而托盘桥架底部每间隔200mm有一道环形加强筋,盖板孔中心与底部环形筋中心对应。……
